


close
Choose Your Site
Global
Social Media


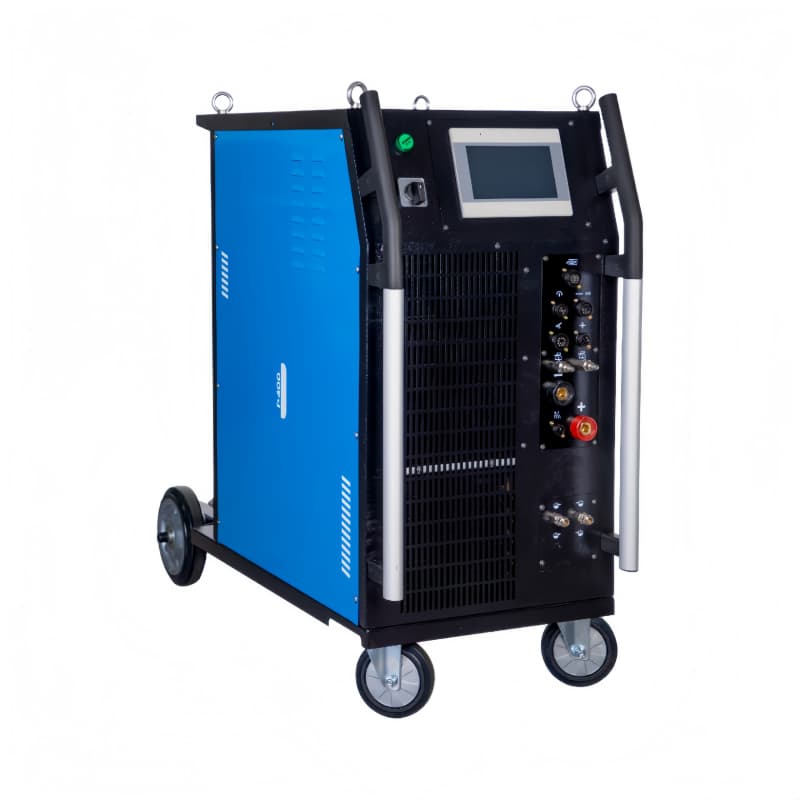


PF800(custom)
BOHAN
Pipe Flange Welding Machine
The flange is seated square on the pipe, the torch travels the joint in one stored program, and the face stays flat enough to check with a straight edge afterwards — not with a hammer and a re-face.
Key Selling Points
- DN50–800 on one machine: spool sizes that normally need three setups
- Heat goes in evenly around the full circumference, so distortion repeats instead of accumulating
- 100 stored programs, recalled by flange size — no re-dialling between jobs
- Water-cooled torch, argon shielded, 60% duty cycle at 400A
Why flange joints get reworked
A manual TIG flange weld fails in one of three ways, and all three are position problems rather than welder skill.
The torch angle drifts as the operator walks around the pipe. The flange is seated a fraction off square before the arc starts. And the heat input changes as the part warms up, so the last quarter of the joint runs hotter than the first. The result passes visual and fails the squareness check, or holds square and leaks at the root on the hydro test.
On a flange welding machine those three variables stop being operator decisions. The torch is held at a fixed angle relative to the joint, the pipe is clamped on centre in a chuck so the flange registers against a machined
face, and the current ramps on a stored program that ends the same way it started. The operator's job becomes: clean the joint, seat the flange, recall the right program.
Technical parameters
Model | PF800 |
Type | TIG weld |
Tube OD range | 50~800mm |
wall thickness | ≤15mm |
Welding process | Wire feeding |
Shielding gas Argon | dual path (inner purge + torch) |
Pre-flow / post-flow | Programmable |
Tilt angle | 0~90° |
Chuck load | 500kg |
Cooling | Water-cooled |
Compatible power source | AW400 |
Welding form | Pipe to pipe ,Pipe to flange,Pipe to elbew |
Cable assembly length | 9.5m |
Through hole diameter | 350mm |
Dimension | 2200x1700x2100mm |
Certification | IS9001 and CE |
Typical applications
- Pharmaceutical & biotech - WFI, purified water and fermentation clean lines, on-site and prefabricated.
- Food & beverage - beer, dairy and juice process piping, filtration skids.
- Data centre & new energy - liquid-cooling manifold piping, batch welded on a production line.
- Aerospace - small-diameter hydraulic and fuel lines.
Detail Shot


How to operate
- Check water, power and argon; clean and align the tube ends.
- Mount the collet insert for your OD and clamp the head on the joint.
- Insert the inner argon plug and start the purge.
- Load the program and close the chamber.
- Weld, then inspect the bead with a borescope.
- PF800 welding unit — 1 set
- Flange fixture / chuck jaws for the quoted flange range — 1 set
- Water-cooled TIG torch with cable — 1
- Argon hose and regulator connection — 1 set
- Spare parts kit: {nozzle, collet body, tungsten, O-rings}}— 1 set
- Operation manual, English — 1
- Tool box — 1
What you get
Standard supply: weld head, one collet insert, 9.5 m cable assembly, water hose set, spare tungsten electrodes, inner argon plug, operation manual, carrying case.
Options: additional collet inserts, AW200 / AW400 power source, remote pendant, spare parts kit.
Delivery: standard configuration ships in 5 working days after receipt of deposit.
Try it on your own tube
Send two 150 mm samples of your actual tube and fitting. We weld them on PF800 and send back the coupons with a borescope video of the inner surface and the parameter report. Five working days, no charge.
What flange sizes can it weld?
DN 50 to DN 600, Outside that range the fixture is made to drawing.


